Welcome to XiYu

Progressive Mold Stamping: How It Works and When to Use It
Learn how progressive mold stamping uses multiple tooling stations to produce precision metal parts efficiently, including benefits, materials, costs, design factors, and suitable applications.

Progressive mold stamping is a high-efficiency metal forming process used to manufacture repeatable sheet-metal components in medium- to high-volume production.
Instead of producing one feature at a time with separate tools, a progressive mold contains multiple stations inside a single mold set. As metal strip moves through the tooling, each station performs a different operation, such as punching, bending, forming, or trimming.
By the time the strip reaches the final station, the finished component can be separated from the carrier strip.
For manufacturers and OEM buyers, progressive mold stamping can provide high production speed, stable repeatability, and competitive unit costs when the part design and production quantity justify dedicated tooling.
However, it is not the right solution for every metal part.
This article explains how progressive stamping works, its main advantages, design considerations, cost factors, and when it should be considered for a custom manufacturing project.
What Is Progressive Mold Stamping?
Progressive mold stamping is a manufacturing process in which a metal strip passes through a sequence of stations within one mold.
Each station performs a specific operation while the strip remains connected to a carrier until the final stage.
Typical operations may include:
| Operation | Purpose | Typical Result |
|---|---|---|
| Pilot / Positioning | Keeps the strip accurately aligned | Stable progression between stations |
| Punching | Creates holes or cutouts | Holes, slots, openings |
| Blanking | Cuts part geometry from sheet | External profiles |
| Bending | Forms the material to an angle | Tabs, flanges, brackets |
| Forming | Creates three-dimensional features | Ribs, channels, contours |
| Coining | Produces controlled local geometry | Fine features or dimensional control |
| Cutoff | Separates the finished part from the strip | Completed stamped component |
The part does not usually become fully formed in a single station.
Instead, its geometry develops gradually as the strip moves through the mold.
This staged approach allows several operations to be integrated into one automated production cycle.
How Does the Progressive Stamping Process Work?
A progressive stamping line generally follows a continuous sequence.
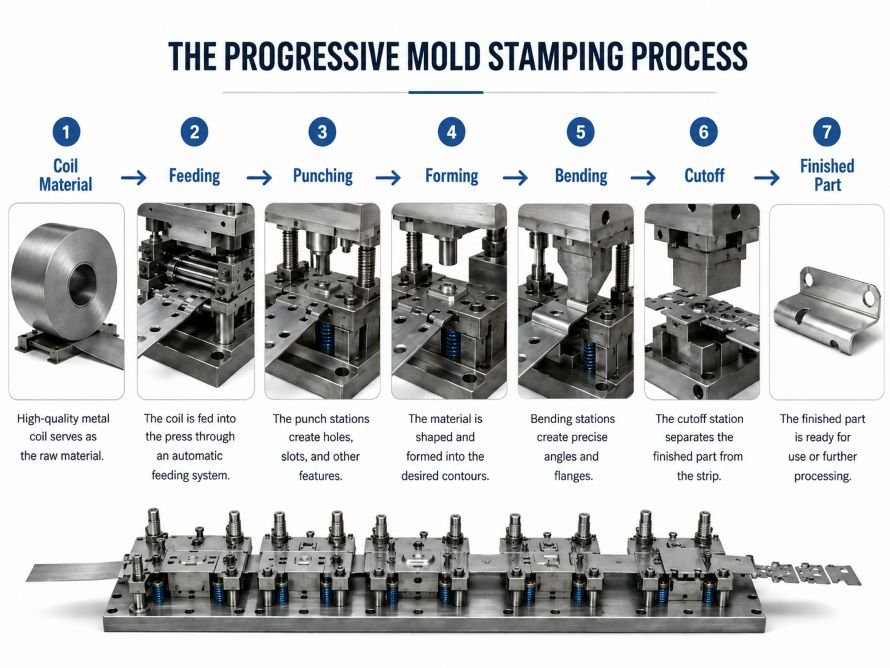
1. Coil or Strip Material Is Fed Into the Press
The process usually begins with sheet metal supplied in coil or strip form.
The material is fed into the stamping press at a controlled pitch.
Accurate feeding is important because every feature produced at later stations depends on the strip arriving at the correct position.
2. The First Stations Create Reference Features
Early stations often punch pilot holes or other reference features.
These help control strip position as the material advances through the tooling.
Good strip guidance is critical because dimensional errors can accumulate if the strip is not positioned correctly at each stage.
3. Multiple Forming Operations Are Performed
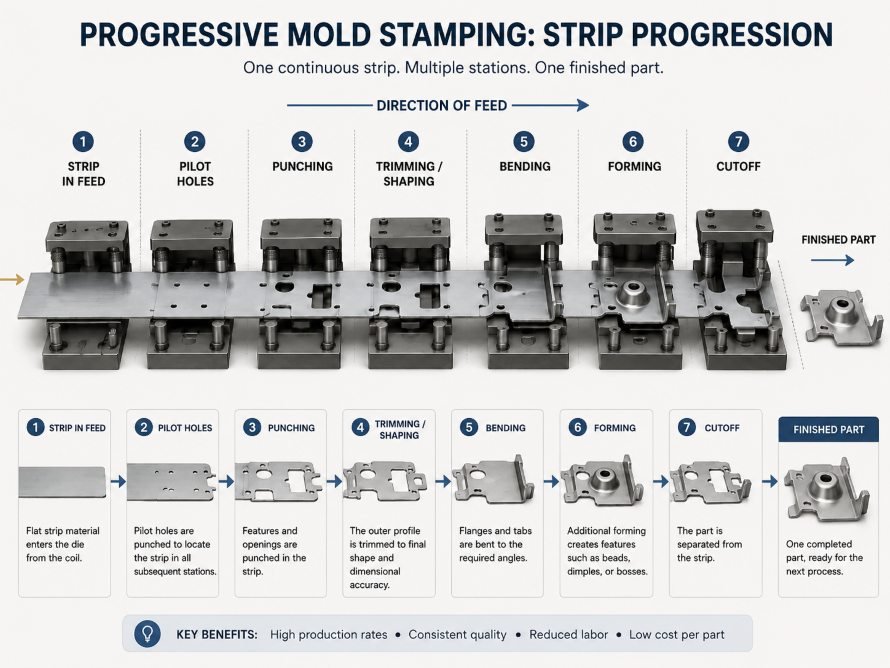
As the strip advances, different stations gradually create the required geometry.
For example:
- Station 1: pilot holes
- Station 2: internal cutouts
- Station 3: external trimming
- Station 4: first bend
- Station 5: second forming operation
- Station 6: final shaping
- Station 7: cutoff
The exact sequence depends on:
- Part geometry
- Material type
- Material thickness
- Tolerances
- Forming difficulty
- Required production speed
A well-designed sequence reduces unnecessary material deformation and helps control part accuracy.
4. The Finished Part Is Separated
At the final station, the completed component is normally cut away from the carrier strip.
Depending on the project, the finished part may then move to:
- Collection
- Deburring
- Washing
- Tapping
- Welding
- CNC machining
- Surface treatment
- Inspection
- Assembly
This makes progressive stamping one part of a broader manufacturing process when secondary operations are required.
What Does a Progressive Mold Look Like?
A progressive mold is usually more complex than a simple single-operation stamping mold.
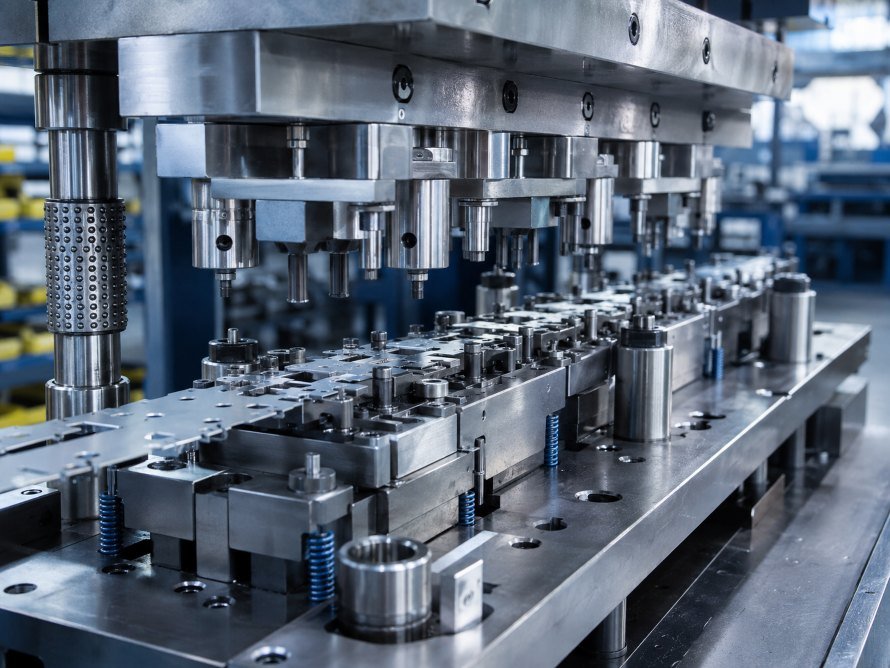
It may include:
- Upper and lower mold plates
- Punches
- Mold inserts
- Guide posts
- Pilots
- Strippers
- Springs
- Lifters
- Stock guides
- Sensors
- Cutoff mechanisms
The metal strip travels through the mold along a carefully designed strip layout.
Each component inside the tooling must work together accurately.
This is why progressive stamping capability depends heavily on tooling engineering, not just press capacity.
Poor tooling design can lead to problems such as:
- Inconsistent dimensions
- Excessive burrs
- Strip misfeeding
- Premature tool wear
- Part deformation
- High scrap rates
- Production interruptions
For high-volume programs, the quality of the mold can have a major influence on long-term manufacturing cost. Because progressive Mold performance depends heavily on engineering and planning, supplier capability should be evaluated carefully. Choosing a precision metal stamping manufacturer in China.
Progressive Mold Stamping vs Single-Operation Stamping
Both methods can produce stamped metal parts, but they are suited to different manufacturing situations.
| Factor | Progressive Mold Stamping | Single-Operation Stamping |
|---|---|---|
| Number of Operations | Multiple operations in one mold | Usually one primary operation per mold |
| Material Flow | Continuous strip moves through stations | Parts may be handled between operations |
| Production Speed | High for suitable parts | Usually lower for multi-step components |
| Tooling Complexity | Higher | Lower |
| Initial Tooling Cost | Generally higher | Generally lower |
| Automation Potential | Very high | Depends on process |
| High-Volume Production | Excellent | Can be less efficient for complex multi-step parts |
| Design Flexibility | Best when geometry suits sequential forming | Useful for simpler or lower-volume operations |
Single-operation tooling can be practical for relatively simple components or lower production requirements.
Progressive tooling becomes more attractive when several operations must be repeated at scale.
What Are the Main Advantages of Progressive Mold Stamping?
High Production Speed
One of the biggest advantages is cycle efficiency.
Because several operations are integrated into one mold, the press can produce components continuously as the strip advances.
This reduces the need to transfer individual parts manually between separate operations.
Stable Repeatability
Once the tooling and feeding system are properly set up, the same sequence is repeated each press cycle.
This supports consistent geometry across large production runs.
Reduced Part Handling
In multi-stage conventional production, partially completed parts may need to be transferred between several machines or mold.
Progressive tooling keeps the component attached to the strip throughout most of the forming sequence.
This can reduce:
- Manual handling
- Work-in-process inventory
- Positioning errors
- Production steps
Multiple Features in One Production System
A progressive mold can potentially combine:
- Holes
- Slots
- Bends
- Tabs
- Embossed features
- Formed geometry
- Cutoff
This integration is one reason progressive stamping can become efficient for complex sheet-metal components.
Lower Unit Cost at Sufficient Volume
Progressive tooling normally involves a higher initial investment.
However, once the production volume becomes large enough, the high production efficiency can reduce the cost per component.
The economic benefit therefore depends heavily on expected production quantity.
What Types of Parts Are Suitable for Progressive Mold Stamping?
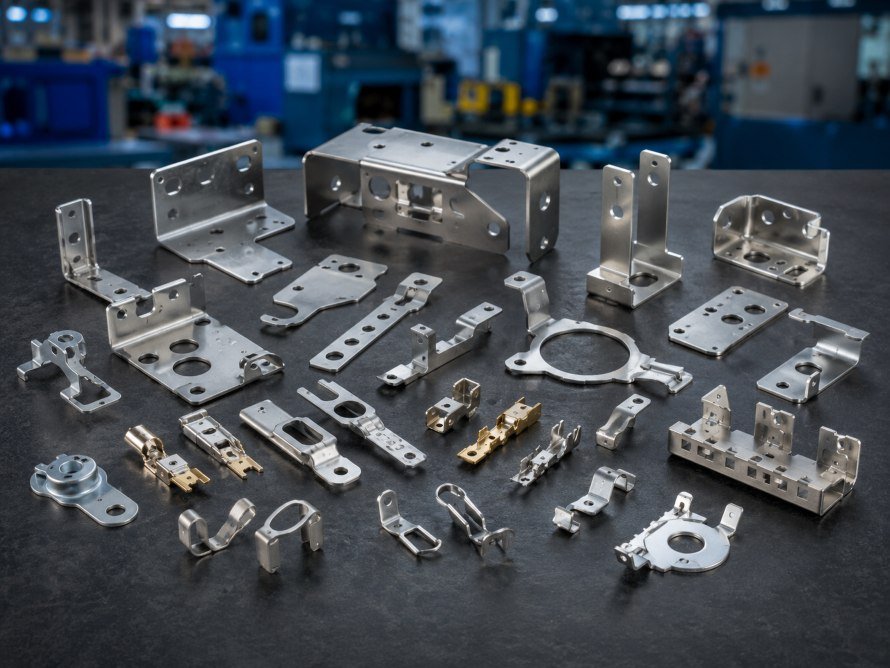
Progressive stamping works particularly well for parts that:
- Are produced from sheet metal
- Require repeat production
- Have multiple punched or formed features
- Can remain connected to a carrier strip during production
- Require medium- or high-volume manufacturing
- Have geometry that can be formed gradually through multiple stations
Typical applications may include:
| Industry | Example Components |
|---|---|
| Electronics | Contacts, clips, shields, brackets |
| Electrical | Terminals, conductive components, connectors |
| Automotive | Clips, mounting brackets, structural hardware |
| Lighting | Brackets, mounting hardware, formed components |
| Machinery | Retainers, supports, connectors |
| Consumer Products | Internal frames, clips, functional hardware |
| Smart Home | Mounting parts, brackets, internal metal components |
The process can also be used for small precision components where repeatability and production speed are important.
What Materials Can Be Used in Progressive Stamping?
Many sheet metals can be used, depending on the geometry and performance requirements of the finished part.
Common materials include:
| Material | Main Characteristics | Common Considerations |
|---|---|---|
| Stainless Steel | Strong, corrosion resistant | Higher forming force and springback |
| Mild / Carbon Steel | Strong and economical | Surface protection may be required |
| Aluminum | Lightweight, corrosion resistant | Surface scratching and springback require control |
| Copper | Excellent conductivity | Material value and softness affect handling |
| Brass | Good formability and conductivity | Often used for connectors and decorative parts |
| Phosphor Bronze | Good elasticity and fatigue resistance | Common for clips and electrical contacts |
Material behavior must be considered when designing each forming station.
Important factors include:
- Tensile strength
- Hardness
- Ductility
- Grain direction
- Springback
- Surface condition
- Material thickness
The same part geometry may require different tooling strategies when produced from different materials.
Why Is Strip Layout Important?
The strip layout defines how the part moves through the progressive mold.
It determines:
- Station sequence
- Material pitch
- Carrier design
- Part orientation
- Scrap areas
- Material utilization
A poorly optimized strip layout can waste material or create unstable forming conditions.
For high-volume production, material utilization becomes especially important because raw material can represent a significant portion of total part cost.
For example, a small improvement in material usage may appear insignificant on one component.
But across hundreds of thousands or millions of parts, that improvement can create substantial savings.
Therefore, strip layout optimization is both an engineering and cost-control consideration.
What Design Factors Should Engineers Consider?
Designing a part for progressive stamping requires more than checking whether it can physically fit inside a mold.
Several factors should be reviewed during DFM.
Hole and Edge Distance
Holes or slots located very close to part edges may cause distortion or tooling difficulties.
Bend Radius
Very small bend radii can increase the risk of cracking, especially with harder materials.
Springback
Some metals partially return toward their original shape after forming.
Tooling may need compensation to achieve the required final angle.
Feature Sequence
The order of punching and forming operations can affect dimensional stability.
Some features must be produced before bending, while others may need to be completed after forming.
Tolerances
Not every dimension requires the same tolerance.
Applying unnecessarily tight tolerances to non-critical features can increase tooling and inspection costs.
Burr Direction
Burr orientation can matter for parts that:
- Slide against another component
- Contact users
- Carry electrical current
- Require cosmetic surfaces
- Enter an assembly
The required burr direction should be considered when developing the stamping sequence.
What Factors Affect Progressive Mold Stamping Cost?
Progressive stamping cost can be divided into two major categories:
initial tooling cost and production cost.
| Cost Factor | Effect on Cost |
|---|---|
| Number of Stations | More stations generally increase tooling complexity |
| Part Geometry | Complex forms require more sophisticated tooling |
| Material | Grade, thickness and material utilization affect cost |
| Tolerances | Tighter tolerances require more precise tooling and control |
| Tooling Material | Tool steel selection affects mold cost and expected life |
| Sensors / Automation | Additional monitoring can increase tooling investment |
| Production Quantity | Higher volumes spread tooling cost across more parts |
| Secondary Processing | Deburring, plating, tapping, machining or assembly add cost |
| Maintenance | Long production runs require planned tool maintenance |
The lowest tooling quotation is not always the lowest total manufacturing cost.
For long-running programs, buyers should also consider:
- Expected tool life
- Maintenance requirements
- Spare inserts
- Production stability
- Scrap rate
- Cycle time
- Tool repair capability
A more robust tool may cost more initially but perform better over the life of the project.
When Does Progressive Mold Stamping Make Economic Sense?
Progressive stamping is most attractive when the production volume is high enough to justify the tooling investment.
A simplified comparison looks like this:
| Project Situation | Progressive Mold Stamping Suitability |
|---|---|
| One-off prototype | Usually low |
| Very small production batch | Often low |
| Repeated medium-volume orders | Potentially suitable |
| High-volume production | Highly suitable |
| Complex part with several stamping operations | Highly suitable if geometry supports it |
| Frequently changing product design | Less attractive before design is stable |
| Stable design with long production life | Very attractive |
There is no universal quantity threshold because the break-even point depends on:
- Tool cost
- Part complexity
- Alternative manufacturing cost
- Material
- Cycle time
- Annual quantity
- Expected product life
For this reason, buyers should provide both the immediate order quantity and expected annual demand during the quotation stage.
Progressive Mold Stamping vs CNC Machining
For some projects, buyers may be deciding between stamping and CNC machining.
The processes have very different cost structures.
| Factor | Progressive Mold Stamping | CNC Machining |
|---|---|---|
| Initial Tooling Investment | High | Usually much lower |
| Cost Per Part at High Volume | Often low | Remains influenced by cycle time |
| Prototype Flexibility | Limited | Very strong |
| Design Changes | Can require mold modification | Usually easier to implement |
| Sheet-Metal Parts | Excellent | Often inefficient |
| Complex Machined Features | Limited | Excellent |
| Production Scalability | Excellent | Requires additional machine capacity |
CNC machining is often useful during prototype development.
Once the design becomes stable and demand increases, a component may become suitable for stamping.
This is one reason manufacturers that can support both processes can help customers transition from prototype to production.
How Is Quality Controlled in Progressive Stamping?
High-speed production requires effective quality control.
Inspection may include:
- Dimensional measurement
- Hole position inspection
- Bend angle inspection
- Flatness checks
- Surface inspection
- Burr inspection
- Material verification
- Coating or plating inspection
However, quality control should also focus on the process itself.
Progressive mold may use sensors to detect conditions such as:
- Misfeeds
- Part presence
- Strip position
- Material feeding issues
Tool wear must also be monitored because worn punches or mold inserts can gradually change part quality.
Preventive maintenance can help reduce unexpected production interruptions and quality problems.
What Should You Include in a Progressive Stamping RFQ?
Providing complete information allows a manufacturer to evaluate whether progressive tooling is appropriate.
| RFQ Information | Why It Matters |
|---|---|
| 2D Drawing | Defines dimensions, tolerances and notes |
| 3D CAD File | Helps analyze forming sequence and geometry |
| Material Grade | Determines forming characteristics |
| Material Thickness | Influences mold clearance and tooling design |
| Annual Quantity | Important for evaluating tooling economics |
| Batch Quantity | Helps plan production strategy |
| Surface Treatment | Defines secondary processes |
| Critical Dimensions | Helps identify precision requirements |
| Application | Helps evaluate functional risks |
| Expected Product Life | Supports tool-life and investment planning |
If annual demand is uncertain, it is still helpful to provide an estimated range.
The manufacturer can then compare different tooling and production approaches.
How to Choose a Progressive Mold Stamping Manufacturer
Progressive stamping depends heavily on tooling expertise.
When evaluating a supplier, buyers should consider more than machine size or press tonnage.
Important capabilities include:
- In-house or controlled mold design
- Tooling manufacturing capability
- Strip-layout engineering
- Material experience
- Press and feeder capability
- Tool maintenance capability
- Quality inspection
- Secondary processing
- Engineering communication
- Production capacity
A strong supplier should be able to explain why a specific stamping sequence is recommended and identify potential manufacturing risks before tooling begins.
Progressive Mold Stamping at Xiyu Hardware
Dongguan Xiyu Hardware & Electronic Co., Ltd. provides custom precision hardware manufacturing services for OEM and ODM projects.
The company’s capabilities include:
- Metal stamping mold design and manufacturing
- Precision metal stamping
- CNC machining
- CNC turning
- Sheet metal fabrication
- Secondary hardware processing
For suitable high-volume components, progressive tooling can be evaluated together with material selection, part geometry, tolerances, and production quantities.
For projects that are still in the prototype stage, alternative processes such as CNC machining or sheet metal fabrication may also be considered before investing in production tooling.
This multi-process capability allows the manufacturing approach to be selected according to the actual requirements of the component.
Frequently Asked Questions About Progressive Mold Stamping
What is the main difference between progressive stamping and regular stamping?
Progressive stamping integrates several operations into one multi-station mold while the metal strip advances automatically through the tooling.
Regular or single-operation stamping may perform one main operation at a time.
Is progressive mold stamping only for very high volumes?
It is most attractive for medium- to high-volume production, but the exact break-even quantity depends on tooling cost, part complexity, alternative manufacturing methods, and expected product life.
Can progressive stamping produce tight-tolerance parts?
Yes, depending on the material, geometry, tooling design, and specific dimensions involved.
Tolerance requirements should be evaluated feature by feature rather than applying unnecessarily tight tolerances to the entire part.
Are progressive mold expensive?
They usually require a higher initial investment than simple stamping tools because several operations are integrated into one mold.
However, the higher production efficiency can reduce unit costs over larger production volumes.
Can a progressive stamped part still require CNC machining?
Yes.
Some projects combine stamping with CNC machining, tapping, welding, surface treatment, or other secondary processes when specific features cannot be produced efficiently inside the stamping mold.
Need Progressive Mold Stamping for a Custom Metal Part?
If your component requires repeat production and includes multiple punched, bent, or formed features, progressive mold stamping may be worth evaluating.
Send us your:
- 2D engineering drawing
- 3D CAD file
- Material specification
- Material thickness
- Critical tolerances
- Surface treatment requirements
- Batch quantity
- Estimated annual demand
Xiyu Hardware can review the project and evaluate whether progressive mold stamping or another manufacturing process is more suitable.